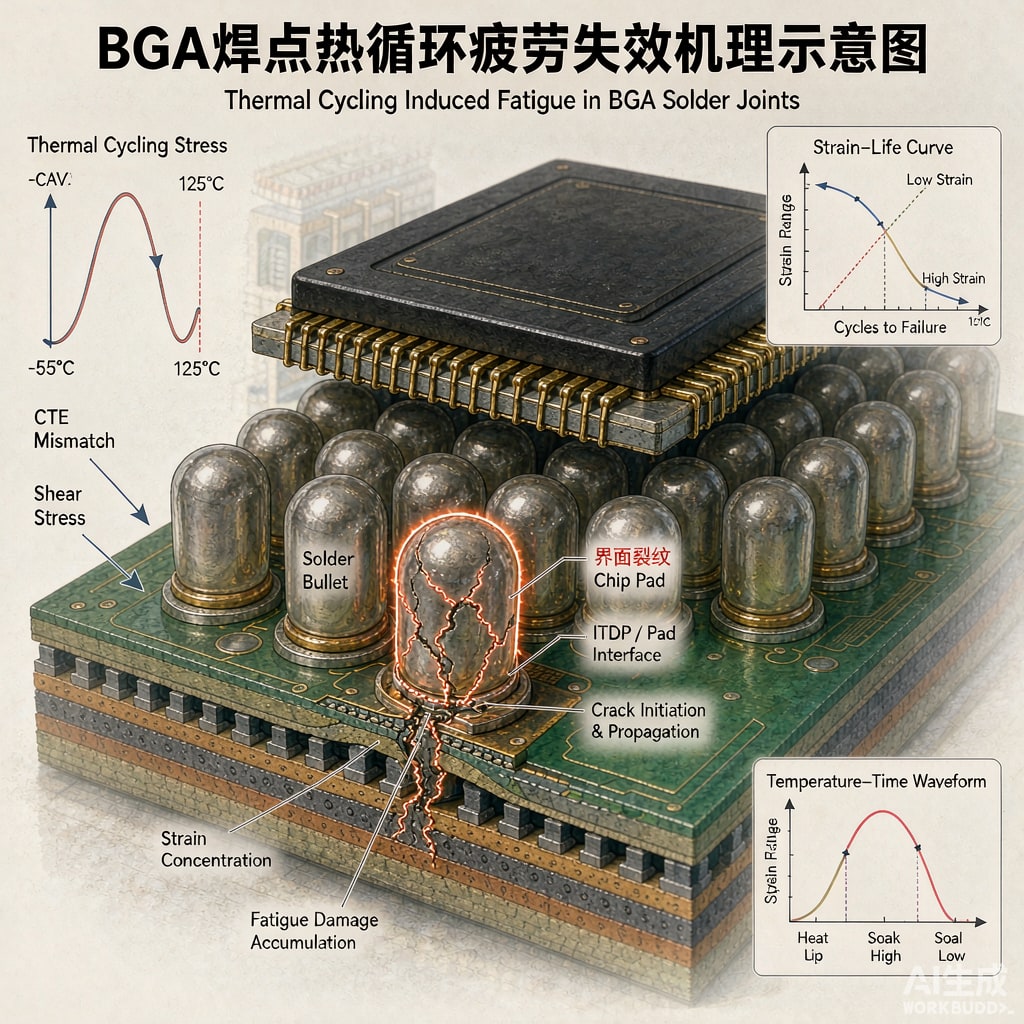
Most SMT boards that pass every functional test still have one Achilles heel: the solder joints that quietly accumulate fatigue damage every time the product heats up and cools down. Power supplies, automotive modules, and anything mounted near a hot component live or die by thermal cycling fatigue. Understanding the mechanics and the standard prediction models turns this from a gamble into a design parameter.
Why Solder Joints Fail in Thermal Cycling
A solder joint co
ects two materials with different coefficients of thermal expansion: the silicon package (about 3 to 7 ppm per kelvin), the FR-4 board (about 14 to 17 ppm in-plane), and, for large components, a metal heat spreader above both. As temperature swings, the mismatch forces the joint to shear cyclically. The damage concentrates in a thin band near the package-to-solder interface, where creep strain accumulates during each dwell at temperature. SAC305 lead-free solder is stiffer and less creep-tolerant than the old leaded alloys, which makes joint geometry and stress relief more important than it was a decade ago.
The Prediction Models: Coffin-Manson and Engelmaier
The industry-standard framework is a Coffin-Manson relationship: cycles to failure scale inversely with a power of the inelastic strain range per cycle. The Engelmaier model makes this usable by estimating the shear strain range from the distance between the component and board neutral points, the CTE mismatch, the temperature swing, and a set of empirically fitted exponents that account for dwell time and frequency.
Inputs You Must Actually Estimate
Three inputs dominate the result. First, the temperature swing delta-T seen by the joint, not the ambient: a component dissipating 5 watts on a poorly spread board can see a local swing two or three times the ambient delta-T. Second, the distance from the neutral point: a BGA with a 25 millimeter body generates far more joint strain than an 0603 resistor, which is why large packages fail first. Third, the effective CTE of the assembly region, which copper planes and stiffeners modify. Getting these three numbers roughly right matters more than polishing the model constants.
Design Rules That Extend Joint Life
Several layout decisions buy fatigue life cheaply. Match pad sizes to the component land pattern specification so the solder fillet forms correctly; an oversized pad does not help and an undersized one concentrates strain. For large BGAs and QFNs, fill via-in-pad structures completely to avoid wicking solder away from the joint, or move vias outside the pad where routing allows. Avoid placing large packages straddling board stiffeners or screw bosses, which locally change the CTE behavior. Add corner-only stochastic underfill or corner bonding for large ceramic packages in high-shock applications. And distribute hot components so no single region of the board dominates the local temperature swing.
The Role of Dwell Time
Creep damage accumulates during the high-temperature dwell, so products with long soaks, like an automotive ECU parked in the sun, are harsher on joints than the same delta-T with short cycles. The model exponents capture this, but the practical takeaway is simple: when you compare your product to test data, match the dwell times or the comparison is meaningless.
Layout Details That Quietly Matter
Beyond package placement, copper plane stitching and thermal relief spokes around thermal pads change the effective stiffness the joint sees. Tie ground planes under large packages with short periodic co
ections so the plane ca
ot bow independently of the package. For co
ectors and edge cards that carry repeated insertion loads in hot environments, specify higher-Tg laminates, because glass transition temperature sets the point where the board CTE climbs steeply and joint strain accelerates. None of these are expensive changes at layout time; all of them are board respins after a field failure.
Accelerated Testing: Plan It Like the Model Expects
Air-to-air thermal cycling per IPC-9701 remains the benchmark test for BGA and chip-scale assemblies. Typical profiles run from minus 40 to plus 125 degrees Celsius with 10 to 15 minute dwells, and sample boards are daisy-chained so resistance monitoring catches failures. Two rules keep the test honest. Keep the ramp rates moderate so the assembly follows the chamber; a ramp so fast the package lags the board measures the chamber, not your design. And report the failure distribution, not just the first failure, because the Weibull slope tells you whether you are seeing a single weak population or a spread of joint qualities.
Reading the Results
Compare measured cycles-to-first-failure against the model prediction at the test profile, then translate to field conditions using the model with the field delta-T and dwell. If the test fails at half the predicted life, suspect solder voiding, poor wetting, or pad cratering rather than the model. Cross-section the failed joints; the crack location, package side versus board side, points directly at which interface to fix.
A Practical Mitigation Checklist
Before release, confirm four things: local delta-T estimates for the hottest large packages, neutral-point distances for every package above roughly 15 millimeters, via-in-pad policy on those packages, and an IPC-9701 test plan whose profile brackets your field environment. Products that pass these four gates rarely surprise anyone in the field, and the ones that do fail give cross-section evidence that points at a fixable root cause instead of a mystery.



