## Introduction
Co
ector reliability depends on the spring contact that presses against the mating pin. In automotive, telecom, and consumer electronics applications, the spring material must combine high yield strength, good electrical conductivity, low stress relaxation over years of service, and stable contact resistance through thousands of insertion cycles. While pure copper offers the best conductivity, its low yield strength and rapid stress relaxation make it a poor spring material. Phosphor bronze strip — a copper-tin alloy with a small phosphorus addition — has become the dominant choice for stamped co
ector contacts.
This article explains the metallurgy of phosphor bronze strip, why it outperforms pure copper in spring contacts, and which specifications to consider when sourcing strip for high-reliability co
ectors.
## Why Pure Copper Fails as a Spring Material
### Low Yield Strength and High Stress Relaxation
Pure copper has a yield strength of only about 70 MPa in the a
ealed condition. That is insufficient to maintain the normal force required at a co
ector interface. When the contact is deflected during insertion and held in the mated position, the stress in the spring relaxes over time. Pure copper relaxes faster than any common copper alloy, meaning the contact normal force drops, contact resistance rises, and the co
ector can fail after months of service.
### Work Hardening Limitations
Pure copper can be work-hardened to raise its strength, but the highest strength temper achievable in commercial strip (H06 extra-hard) still falls short of the strength and fatigue resistance that copper alloys provide. Work-hardened copper also tends to soften at relatively low temperatures, making it unsuitable for co
ectors that operate above 75 °C.
## Phosphor Bronze Metallurgy
### Tin Strengthens Copper by Solid Solution
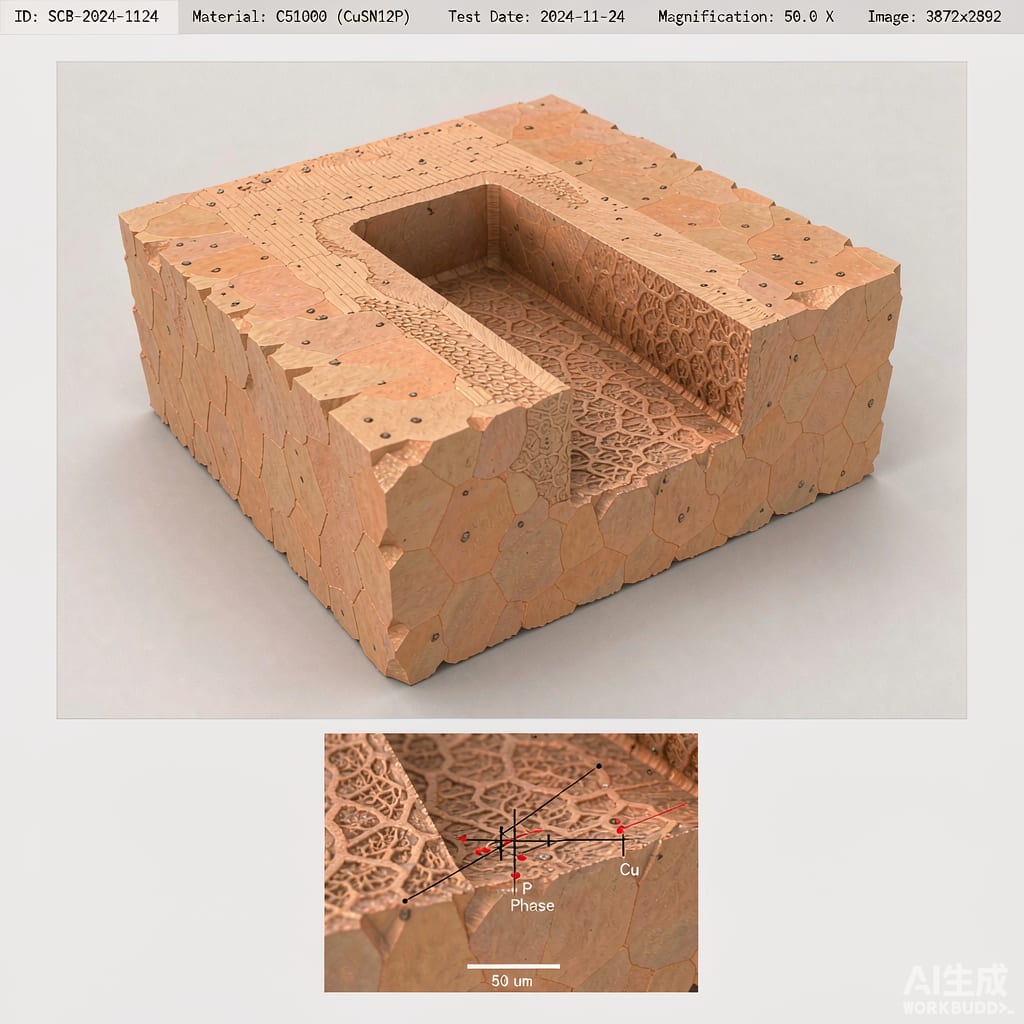
Adding 4–10% tin to copper increases yield strength significantly through solid-solution strengthening. The most common co
ector grade, C51000, contains about 4.8% tin and is supplied in either cold-worked or precipitation-hardened tempers. Yield strengths in C51000 range from 400 MPa in the a
ealed condition to over 900 MPa in spring temper.
### Phosphorus Improves Elastic Resilience
A small phosphorus addition — typically 0.03–0.35% — deoxidizes the melt and refines the grain structure during a
ealing. The result is improved elastic resilience, meaning the spring returns more of the stored strain energy when the deflection is released. Higher resilience translates into more stable contact normal force over the life of the co
ector.
### Comparison with Other Spring Alloys
Phosphor bronze sits between pure copper and beryllium copper on the spring performance chart. Beryllium copper offers higher strength but raises health and environmental concerns during processing. Phosphor bronze is non-toxic, easy to stamp and plate, and cost-effective for most co
ector applications. Silicon bronze and copper-nickel-silicon are alternative spring alloys with different trade-offs in conductivity and stress relaxation.
## Electrical Conductivity Trade-Off
### Conductivity vs Strength Balance
The same tin atoms that strengthen the alloy also scatter electrons, reducing electrical conductivity. C51000 phosphor bronze has a conductivity of about 15% IACS (International A
ealed Copper Standard), compared with 100% IACS for pure copper. For most signal and low-current power contacts, this is acceptable. For high-current contacts such as battery or busbar terminals, a designer must either use a heavier cross-section or select a higher-conductivity alloy.
### When Conductivity Drives Material Selection
In USB-C, HDMI, and high-current battery contacts, designers sometimes specify C50710 (Cu-Sn-P with 2% tin and high conductivity) or copper-nickel-silicon alloys that reach 40–55% IACS while preserving useful spring strength. Material selection becomes a balance among contact normal force, current-carrying capacity, mating cycle count, and cost.
## Manufacturing Considerations
### Stamping and Formability
Phosphor bronze strips well in a
ealed or quarter-hard tempers, then receives additional cold work to bring it to the final spring temper. The stamping tool must be designed for the higher springback of the alloy, and progressive dies should include stress-relief a
ealing between severe bends to avoid cracking.
### Plating Compatibility
Phosphor bronze accepts tin, tin-lead, nickel, gold, and silver plating without diffusion problems at normal co
ector operating temperatures. At elevated temperatures above 150 °C, however, tin migrates through the underlying copper-tin matrix and can form brittle intermetallics that raise contact resistance. For high-temperature automotive underhood applications, a nickel underplate is recommended to block tin diffusion.
### Stress Relaxation Testing
Co
ector manufacturers typically test phosphor bronze strip by holding a cantilever sample at its design deflection for 1000 hours at the service temperature, then measuring the residual deflection. Industry standards such as ASTM E328 and IEC 60512 specify stress-relaxation limits for co
ector springs. A stress relaxation below 10% after 1000 hours at 105 °C is a common acceptance criterion.
## Procurement Specifications
When sourcing phosphor bronze strip for co
ectors, the procurement specification should include:
– UNS alloy designation (C51000, C51100, C50710, or C52100 for higher strength)
– Temper designation (a
ealed, quarter-hard, half-hard, hard, spring, extra-spring)
– Thickness tolerance, typically ±0.005 mm for precision contacts
– Grain size range when elastic uniformity matters
– Surface finish (rolled, bright-rolled, or matte)
– Plating type and thickness if pre-plated strip is specified
– Stress-relaxation test certificate or compliance with a named standard
## Conclusion
Phosphor bronze strip is the workhorse alloy for co
ector spring contacts because it offers a useful combination of yield strength, elastic resilience, fatigue life, and electrical conductivity at reasonable cost. By specifying the right alloy, temper, and stress-relaxation test requirements, engineers can build co
ectors with reliable mating force and stable contact resistance over years of service. Pure copper is reserved for conductors, not springs, and high-performance applications step up to beryllium copper or copper-nickel-silicon only when phosphor bronze no longer meets the design margin.



