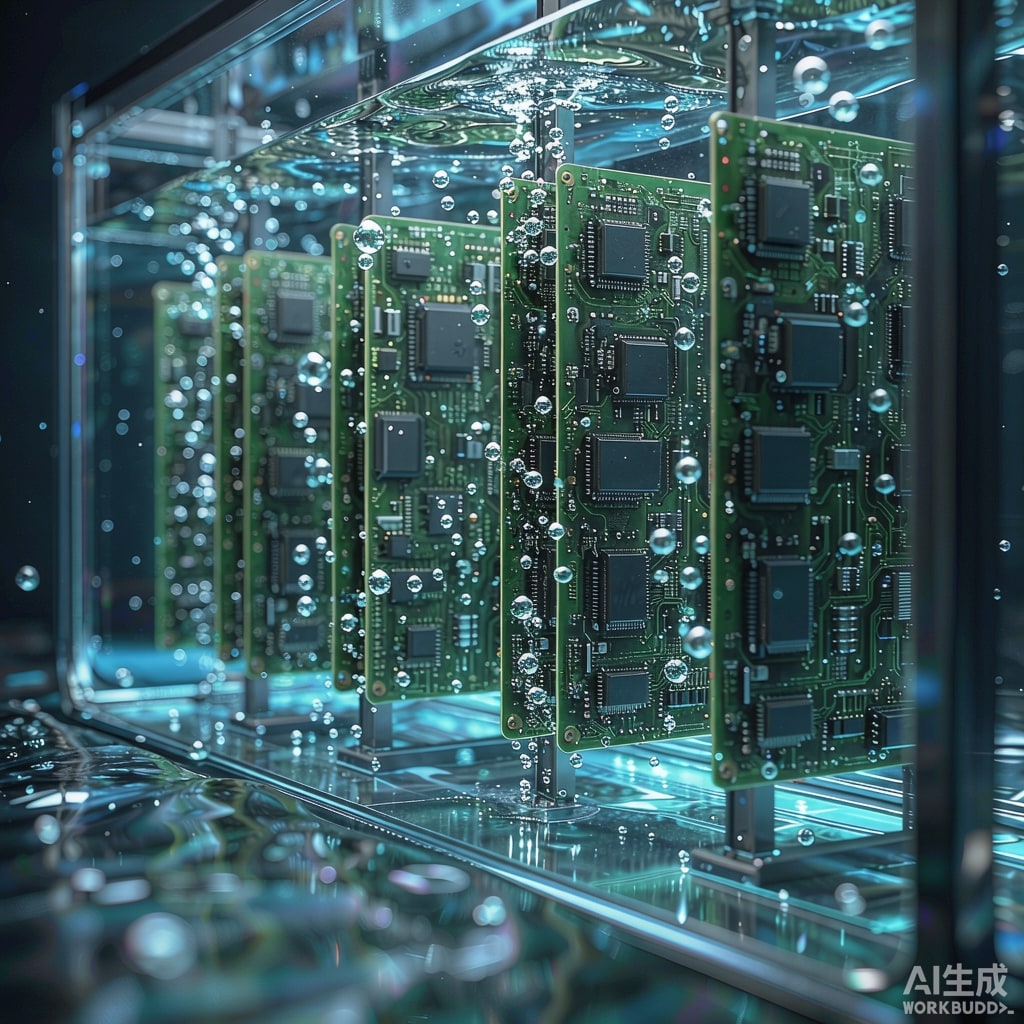
Air cooling has been stretched to its practical limit by accelerator and AI inference boards that dissipate 400 to 800 watts per unit in dense form factors. Rear-door heat exchangers and direct-to-chip cold plates buy time, but two-phase immersion cooling takes a different path entirely: submerge the assembled SMT board in a boiling dielectric fluid and let phase change carry heat away at nearly constant temperature. The physics is compelling, and so is the list of SMT-specific gotchas.
How Two-Phase Immersion Works
The board sits in a sealed tank filled with a low-boiling-point dielectric, typically a fluorinated fluid boiling between 49 and 61 degrees Celsius. Hot component surfaces nucleate bubbles; the vapor rises, condenses on a water-cooled coil at the tank top, and drips back as liquid. Because boiling absorbs roughly 100 kilojoules per kilogram of fluid (latent heat), a modest circulation removes enormous heat flux. Surface temperatures pin near the fluid’s saturation point plus a small superheat — often 55 to 70 degrees Celsius at the silicon, which is a gift to junction reliability compared with the 80 to 100 degree case temperatures of air-cooled designs.
Heat removal capability scales with fluid vaporization dynamics, not with fin area, so 3D-stacked modules and PCBs with components on both faces lose their usual cooling penalty. Rack densities of 30 to 100 kW become routine, and acoustic noise nearly disappears because there are no fans at all.
Fluid Selection and Material Compatibility
The dominant fluids are engineered fluorocarbons: perfluoropolyether and fluoroketone classes. Key selection criteria are boiling point (match to your target junction temperature — 50 degree fluids suit maximum-Tj silicon, 60 degree fluids reduce chiller load), global warming potential, and material compatibility. The compatibility list is where SMT teams get surprised. Fluorinated fluids are excellent solvents for flux residues and many conformal coating chemistries. No-clean flux residues that survive twenty years in air will slowly dissolve in the tank, contaminating the fluid and redepositing on cold surfaces.
Silicone-based conformal coatings swell in fluorocarbons and should be avoided or replaced with fluoroacrylate or parylene coatings qualified for immersion service. Standard FR-4 laminate is generally fine, but low-cost laminates with high moisture absorption will outgas bubbles that interfere with boiling. Electrolytic capacitors with vented rubber seals lose electrolyte fractionally faster; most tank vendors publish approved component lists, and procurement should treat those lists as binding.
SMT Process Changes You Ca
ot Skip
Migration to immersion changes assembly quality gates more than it changes the assembly itself, but the changes are mandatory. First, flux residue management: either switch to a fully water-washable flux process with verified ionic cleanliness below 1.5 micrograms per square centimeter of sodium chloride equivalent, or use a no-clean chemistry specifically certified insoluble in the target fluid. Second, conformal coating becomes selective, not blanket — coat co
ectors and silver-bearing surfaces to prevent fluid chemistry interactions, while leaving boiling-critical hotspots bare so the fluid can nucleate directly on the package.
Third, component marking inks: laser marking survives; solvent-based screen-printed date codes will slowly wash off into the tank. Fourth, tin whisker and tin pest risk profiles change little, but solder joint thermal cycling is gentler because junction temperatures are lower and gradients are smaller — reliability engineering usually finds immersion boards outlast their air-cooled twins on solder fatigue, with electromigration risk unchanged.
Tank-Level Engineering
The condenser loop is the operational heart. Water-side fouling quietly degrades condensation and lets tank pressure and fluid temperature creep upward, so specify redundant condenser circuits with differential-pressure monitoring. Vapor containment matters for both fluid conservation and workplace safety: modern tanks capture over 99.9 percent of vapor with demister pads and positive pressure control. Fluid loss rates in well-run systems run under 1 percent of volume per year; poorly maintained tanks can lose 10 percent.
Monitoring belongs in the automation scope: fluid level, saturation pressure, dissolved water content, and boil-image cameras that spot dry-out on high-flux surfaces. Dry-out — where a hotspot gets so hot that a stable vapor blanket forms — is the fundamental failure mode of pool boiling, and mitigating it means keeping local heat flux below the fluid’s critical heat flux, typically 15 to 25 watts per square centimeter for these fluids. Devices that exceed that limit need embedded heat spreaders or local jet enhancement rather than relying on bare boiling.
When Two-Phase Makes Business Sense
Fluorinated fluids cost hundreds of dollars per liter, so fluid inventory dominates capital cost for small deployments. The economics work best above roughly 50 kW per rack, in hot climates where chiller energy is expensive, and in applications where noise or floor space is binding. For a Southeast Asian build site, the chiller load reduction alone often pays back the fluid premium within three to five years. Start with a single engineering tank on a board family that already fails thermally in air, build the compatibility test matrix, and scale only after a full quarter of operating data — two-phase immersion rewards disciplined operators and punishes improvised ones.



