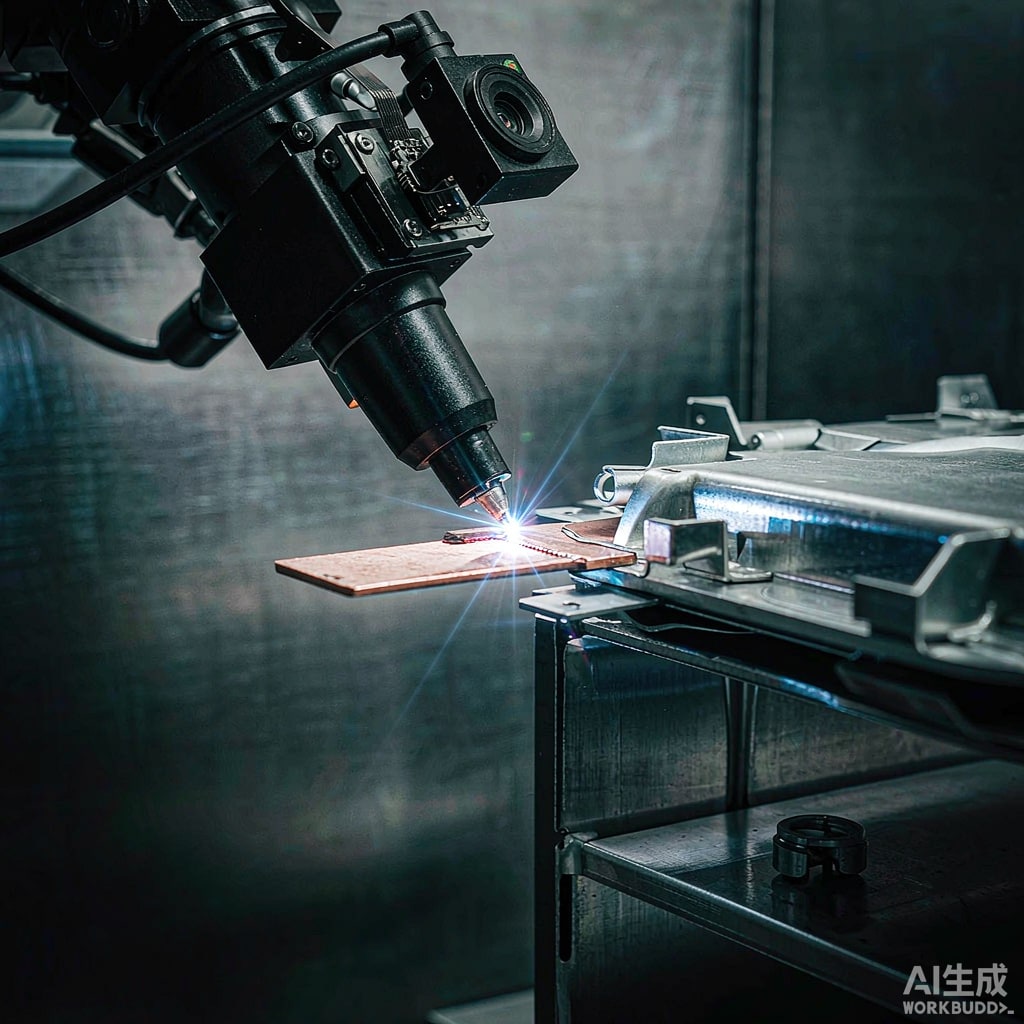
Joining copper strip sections into finished SMT busbar assemblies is one of the most consequential process decisions in power electronics manufacturing. The joint carries the full load current, must survive thermal cycling, and adds contact resistance to a path where milliohms matter. Choosing between resistance welding, laser welding, ultrasonic bonding, and soldering is not a matter of preference — each has a defined process window, metallurgy, and failure mode profile.
Why Copper Strip Joints Matter in SMT Power Assemblies
A laminated busbar or stamped copper strip assembly in a power converter may carry hundreds of amps. A poorly made joint concentrates current at contact asperities, raising local temperature and accelerating degradation. Every joint should therefore be evaluated on three criteria: joint resistance (typically specified below 50 µΩ for large busbars), shear and peel strength, and stability under thermal cycling between −40°C and +125°C.
Copper’s excellent thermal conductivity — 400 W/m·K — makes it forgiving of localized heating during joining, but also means heat spreads quickly into adjacent insulation or nearby components. Process choice must account for heat-affected zone (HAZ) control, especially near polymer spacers or soldered component terminals.
Resistance Welding for Copper Strip Tabs
The Conductivity Problem
Copper is difficult to resistance weld because its resistivity (1.7 µΩ·cm) is far below that of steel. Welding heat is generated by I²R, and most of the resistance in a copper joint sits at the faying surfaces, not the bulk. Practical resistance welding of copper strip therefore relies on:
- Electrode force of 1.5–4 kN to break surface oxide
- Short weld times (20–80 ms) with medium-frequency DC power
- Surface plating (tin or nickel) that raises interfacial resistance and enables consistent nugget formation
For bare C11000 copper-to-copper joints, projection welding is often used instead of spot welding: small projections pre-formed on one strip concentrate current and provide repeatable weld initiation. Nugget diameters of 2–4 mm are typical for 0.5–1.5 mm strip, producing tensile-shear strengths of 1–2 kN per weld.
Electrode Selection
RWMA Class 2 (Cu-Cr-Zr) electrodes are standard. Copper electrodes that contact copper strip need frequent dressing (every 500–1,000 welds) because alloying and pick-up degrade the contact face. Spherical electrode radii of 50–75 mm give the best nugget-to-mark ratio on thin strip.
Laser Welding: Precision and Speed
Fiber laser welding (1,070 nm wavelength) is increasingly the default for copper strip joining in battery tabs, busbar splices, and co
ector assemblies. Copper’s reflectivity at 1 µm is above 95% when cold, which creates a startup instability: the beam must couple into the surface before meaningful absorption begins. Modern solutions include:
- Green laser sources (532 nm): absorption at room temperature rises from ~5% to ~65%, giving stable keyhole formation with lower power
- Blue lasers (450 nm): even higher absorption, ideal for thin foil-to-strip joints
- Ring-mode beams: a low-power core preheats while the ring delivers the forming pulse, stabilizing the transition from reflection to keyhole
Typical parameters for 0.8 mm copper strip lap joints: 3–6 kW peak power, 0.1–0.3 mm focal offset below surface, welding speed 50–150 mm/s, shielding with argon or nitrogen. Penetration depth tolerance of ±0.1 mm is achievable with real-time photodiode monitoring.
Quality Control
Laser welds on copper are inspected by cross-sectioning for first-article qualification and by inline monitoring (photodiode signal deviation, or coaxial thermal imaging) for production. Key defects are spatter, porosity from dissolved hydrogen, and lack-of-fusion at the root — all detectable through process-signal signatures rather than post-process X-ray.
Ultrasonic Metal Welding for Thin Tabs
Ultrasonic welding joins 0.05–0.4 mm copper foil and strip to terminals at temperatures below 40% of the melting point, making it the preferred process for lithium-ion cell tabs and flexible busbar assemblies. A 2–3 kW 20 kHz system welds overlapping strip layers under 0.3–0.6 MPa tip pressure for 0.1–0.5 s.
The joint is a solid-state bond formed by oxide disruption and microwelding at asperities. Electrical resistance across an ultrasonic copper joint is near-bulk (under 20 µΩ) and mechanical strength increases with weld energy until tip penetration limits are reached. The process handles dissimilar stacks — copper strip to nickel-plated steel, aluminum, or brass — without intermetallics, which is its decisive advantage over soldering in mixed-material assemblies.
Soldering Copper Strip Assemblies
Soldering remains the most equipment-friendly option and integrates naturally with SMT reflow when the copper strip is part of a PCB-level assembly. Design considerations:
- Alloy selection: SAC305 (Sn-3.0Ag-0.5Cu) for standard reflow; SnCu1 for cost-sensitive wave joints; SnBiAg low-temperature alloys when nearby components are temperature-limited
- Copper dissolution: during reflow, copper dissolves into liquid tin at roughly 0.1 µm per 10 seconds above 240°C. Thick strip is unaffected, but 0.1–0.2 mm strip joints on long profiles need profile time limits
- Current path: a solder joint’s current rating is roughly 3–5 A per mm² of wetted cross-section — for busbar currents, solder is used for mechanical registration and sealing while bulk current flows through welded or pressed contacts
Flux residues on power assemblies must be low-ionic (J-STD-004 ROL0 or RE0) because leakage current across insulation in humid environments degrades clearance compliance.
Selection Guide
Choose resistance/projection welding for high-volume stamped strip assemblies with plated surfaces. Choose laser welding when precision, speed, and a narrow HAZ justify capital cost — the standard for EV battery and power module busbars. Choose ultrasonic welding for thin foil-to-terminal joints and mixed-metal stacks. Use soldering when the strip joint must be reworkable, sealed, or produced with SMT-line equipment. Validating the choice with cross-sections, microhardness mapping, and thermal cycling (IEC 60068-2-14, 500 cycles) before locking the process will prevent field failures that no post-assembly inspection can catch.



