Why Bending Defines Terminal Quality
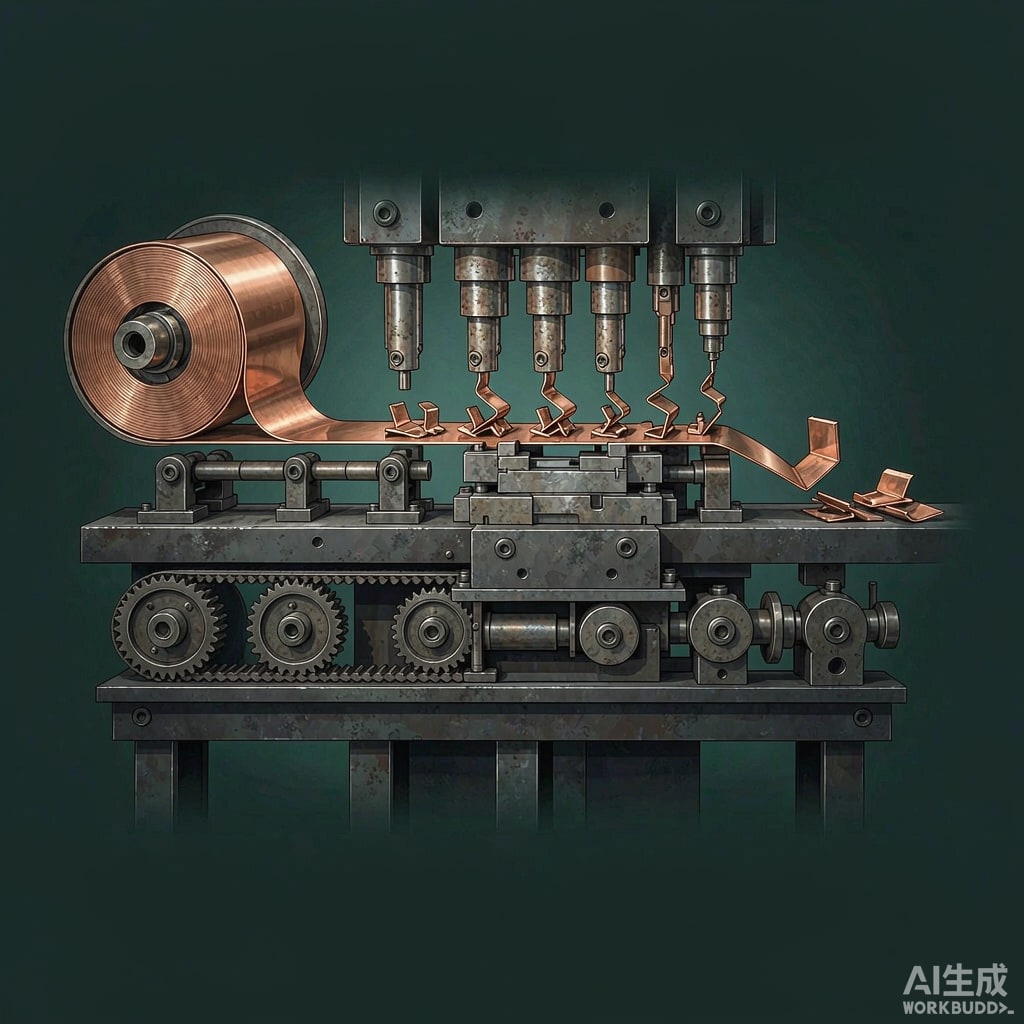
Most SMT terminals, spring contacts, battery tabs, and shield clips begin as flat copper strip and reach their final shape through one or more bends. A 90° form on a battery contact, a Z-bend on a shield can spring leg, or a hemmed edge on a co
ector lug all concentrate strain in a narrow outer-fiber zone. When the copper strip, its temper, or the bend orientation is chosen poorly, that zone cracks — sometimes immediately on the press, sometimes weeks later in the field as fatigue progresses from micro-cracks. Understanding minimum bend radius and grain direction is therefore as important as alloy selection for any formed SMT contact.
Temper and Its Effect on Formability
From A
ealed to Full-Hard
Copper strip is supplied in tempers ranging from a
ealed (soft) to spring hard, and each step up in hardness trades formability for strength:
- A
ealed (O60/O50):
Elongation above 30%; bends with essentially zero inside radius. Used where deep forming matters, but yield strength is low, so finished parts dent and lose contact force. - 1/2 hard (H02): A common compromise for stamped terminals — enough strength for contact force, yet able to take 90° bends at an inside radius of roughly 1× to 2× material thickness.
- Full hard (H04) and spring temper (H08): High yield strength for spring contacts, but bend radii of 2× to 4× thickness or more are required, and bending parallel to the grain becomes risky.
Precipitation-strengthened alloys such as CuNiSi (C7025) and CuNiSn follow the same logic, but their high-strength tempers demand larger radii and careful bend-axis control.
Grain Direction and Anisotropy
Bending Across vs With the Rolling Direction
Rolled copper strip has an elongated grain structure. Bends made perpendicular to the rolling direction (bend axis parallel to rolling direction, forming across the grain) stretch the material uniformly and tolerate the smallest radii. Bends made parallel to the rolling direction (forming with the grain) concentrate strain along grain boundaries and at elongated inclusions, so crack resistance can drop by 30–50% for the same temper.
In strip-fed progressive dies the bend axis orientation is fixed by the part layout — you ca
ot rotate the coil. This means the part drawing should specify which bend axes are parallel or perpendicular to the coil feed direction, and the strip must be quoted and tested in that orientation. A strip qualified only with transverse bend samples may fail when the die bends along the grain.
Minimum Bend Radius Guidelines
A practical starting point is the radius-to-thickness ratio (R/t) measured on the inside of the bend:
- C11000 electrolytic tough pitch, a
ealed:
R/t ≈ 0.5 across the grain; 1.0 with the grain. - C11000, 1/2 hard: R/t ≈ 1.0–1.5 across the grain; 2.0 with the grain.
- C19400 or C19700, hard temper: R/t ≈ 2.0 across the grain; 3.0–4.0 with the grain.
- C17200 beryllium copper, 1/2 hard: R/t ≈ 1.5–2.0; full hard demands 3.0 or greater plus careful edge preparation.
- Brass (C26000), 1/2 hard: R/t ≈ 1.5–2.0; brass is notably notch-sensitive, so edge quality dominates.
These are design guides, not guarantees — always verify with 90° bend samples cut in the production orientation, then add margin for plating and handling.
Preventing Cracks in Production
Edge Quality, Burr Side, and Die Clearance
Most field cracks do not start at the center of the bend face; they start at the strip edge or at a punched hole inside the bend zone. Slit edges carry a burr and a work-hardened fracture zone that act as stress concentrators. Three practices control this:
- Put the burr inside the bend: Orient the blank so the punched burr faces the inside radius. A burr on the stretched outer fiber can halve bend life.
- Keep the slitter edge out of bend zones: Where layout allows, position bend lines at least 2–3× thickness away from slit edges.
- Spec deburred or drawn edges: For tight radii on spring alloys, request edge-dressed strip or a light edge rolling pass.
Where a tight bend is unavoidable on a high-strength temper, warm forming (150–250°C) restores ductility locally without a
ealing the whole part.
Plating and Post-Form Sequencing
Tin, nickel, and gold plating add thin, hard layers that crack if bent after plating. Form-then-plate is the reliable sequence for tight radii; if plating must follow blanking but precede forming, increase the bend radius by one R/t step to compensate for the reduced outer-fiber ductility.
Specifying Strip for Bent SMT Parts
A complete forming specification includes alloy and temper, thickness tolerance, edge condition, bend-axis orientation on the drawing, minimum bend test (e.g., 90° bend over a mandrel at R/t 1.0 with no visible cracking at 10× magnification), and plating sequence. Suppliers can certify bend test results per coil lot when this is written into the purchase specification, converting formability from a hope into a measured property.
Conclusion
Crack-free SMT terminals come from three aligned decisions: a temper matched to the contact-force requirement, a bend radius chosen from R/t rules for that temper, and a layout that respects grain direction and edge condition. Respecting these rules at the design stage costs nothing; discovering them on a 60-ton progressive die costs a tooling rework and weeks of schedule.



