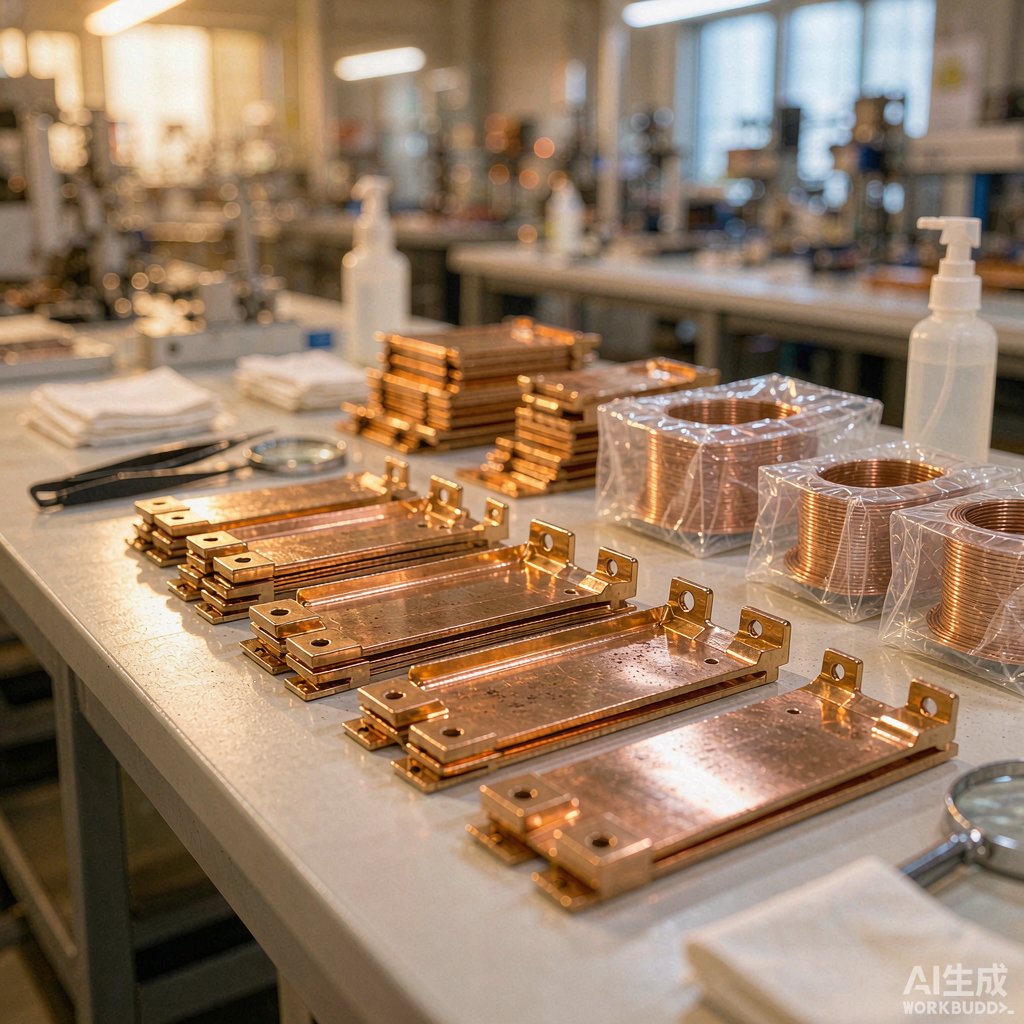
Bare copper strip arrives from the mill bright and mirror-like, yet stamped contacts that sit in a warehouse for a few months often come out dull, brown, or even purple. That color change is tarnish: thin films of copper oxide and copper sulfide that raise contact resistance and degrade solderability. For SMT stamped parts such as spring contacts, fuse clips, battery tabs, and co
ector terminals, tarnish control is just as important as alloy selection. This guide explains how tarnish forms, how it affects assembly yield, and which passivation, plating, and packaging choices keep copper strip stable from mill coil to reflow oven.
How Copper Strip Tarnishes in Storage
Copper reacts continuously with oxygen, moisture, and sulfur-bearing gases in the air. At room temperature a cuprous oxide (Cu2O) film starts growing within hours and reaches tens of nanometers over weeks. The reaction rate roughly doubles with humidity above 60 percent RH, and it accelerates sharply wherever sulfur-bearing gases are present. Hydrogen sulfide and sulfur dioxide at parts-per-billion levels are enough to discolor copper and to turn silver plating black through silver sulfide formation.
Common Environmental Drivers
- Humidity above 60 percent RH, which creates the thin water film that ions need to move across the surface.
- Sulfur sources such as industrial air, vulcanized rubber bands and gaskets, some cardboard grades, and certain wooden pallets.
- Chlorides from fingerprints, sweat, or coastal air, which seed localized pitting and green corrosion.
- Temperature cycling, which pumps moisture in and out of packaging and accelerates film growth.
Brass strip follows the same chemistry but discolors more slowly because zinc at the surface slows oxide growth; its main long-term risk in wet conditions is dezincification rather than simple tarnish.
How Tarnish Affects SMT Stamped Parts
Tarnish films are only tens to hundreds of nanometers thick, but at electrical contact scales that is a lot. Copper oxide is a semiconductor, and its effective film resistance grows quickly with thickness, contact force, and current level. In soldering, flux must chemically remove the oxide layer before solder can wet the base metal; heavy tarnish consumes flux capacity and leaves non-wetting or de-wetting patches.
Contact Resistance Drift
For low-voltage, low-force contacts such as memory card springs and battery tabs, a visible brown film can push milliohm-level contact resistance into the tens of milliohms. Wiping contacts scrub off some film during insertion, but static contacts, spring fingers under shields, and lightly loaded tabs have little wiping action and show the worst drift. Unstable contact resistance shows up later as intermittent signals, CRC errors, and random resets that are expensive to debug in the field.
Solderability Failures and Reflow Defects
Heavily tarnished tab and terminal surfaces produce classic assembly defects: non-wetting leads, dull grainy solder fillets, voided joints, and skip-solder on the opposite side of through-hole pins. Because surface-mount terminals are soldered by mass reflow with fixed flux volume, there is little chance to rework a single bad part. Solderability is therefore audited on incoming strip and finished parts using wetting-balance or dip-and-look methods referenced in IPC solderability standards.
Passivation Options That Preserve Solderability
The goal of passivation is a film thin enough to block corrosion gases yet penetrable by mild flux during soldering. The main options for copper and brass strip are:
- Benzotriazole and tolyltriazole treatments (BTA/BTAT): the industry standard. These form a nanometer-scale complex with copper that is invisible, does not affect stamping, and remains solderable with standard no-clean and water-wash fluxes.
- Long-chain organic inhibitors: thiol- and amine-based films that add lubricity for high-speed stamping; these usually need degreasing before plating or welding.
- Chromate-free conversion coatings: modern replacements for traditional chromates, which are restricted under RoHS and similar regulations.
- Mill antioxidant coatings: light wax or stearate films applied at the rolling mill for coil storage; effective for strip, but they must be removed before plating, brazing, or wire bonding.
- Pre-plated strip: tin, nickel, silver, or nickel-then-gold over the copper completely stops tarnish at the source and is the most robust choice for contact surfaces that must stay bright for twelve months or more.
Choosing Between Bare-Passivated and Pre-Plated Strip
A practical decision rule: parts wiped by the mating contact and consumed within six months usually survive fine with BTA-passivated bare copper or brass. Parts with static, low-force contact surfaces, long warehouse life, or soldering-critical tabs justify the cost of tin or nickel plating applied on the strip before stamping. Plating the coil rather than dip-plating loose parts also protects the stamped edges, which are where bare-strip corrosion usually starts.
Packaging and Warehouse Controls
Passivation only works if the storage environment cooperates. The highest-return controls are inexpensive:
- Seal coils and stamped parts in vapor corrosion inhibitor (VCI) paper or bags, ideally with desiccant.
- Hold the warehouse below 40 percent RH where possible; avoid storing strip near washers, plating lines, or loading docks with humid outside air.
- Keep rubber bands, rubber matting, and fresh cardboard away from bare copper surfaces.
- Use gloves during handling so fingerprints do not seed chloride corrosion.
- Apply first-in, first-out discipline: six to twelve months shelf life is a realistic pla
ing number for bare-passivated strip, and one to two years for pre-plated strip.
Verifying Tarnish Resistance Before Release
Tarnish resistance should be specified and verified, not assumed. A short qualification package includes humidity chamber exposure (for example 40 degrees C at 93 percent RH) with visual grading at 24, 96, and 240 hours; sulfur or hydrogen sulfide gas exposure for silver-plated contacts; wetting-balance solderability checks before and after storage simulation; and periodic contact-resistance trending on retained stamped samples. Plants that track these four numbers rarely meet tarnish surprises; plants that do not track them usually meet them twice a year, in summer.
Conclusion
Copper strip tarnish is predictable surface chemistry, and it is fully manageable with three coordinated decisions: mill-level passivation or pre-plating matched to the contact duty, sealed low-humidity packaging, and a small verification routine on incoming and outgoing parts. Suppliers who can document BTA passivation levels, plating thickness, and humidity test data make that coordination much easier. TechMartSe supplies copper, brass, and plated strip products with passivation and plating options, plus technical datasheets that help Southeast Asian electronics manufacturers keep stamped SMT contacts bright, solderable, and low-resistance from the coil to the reflow oven.



