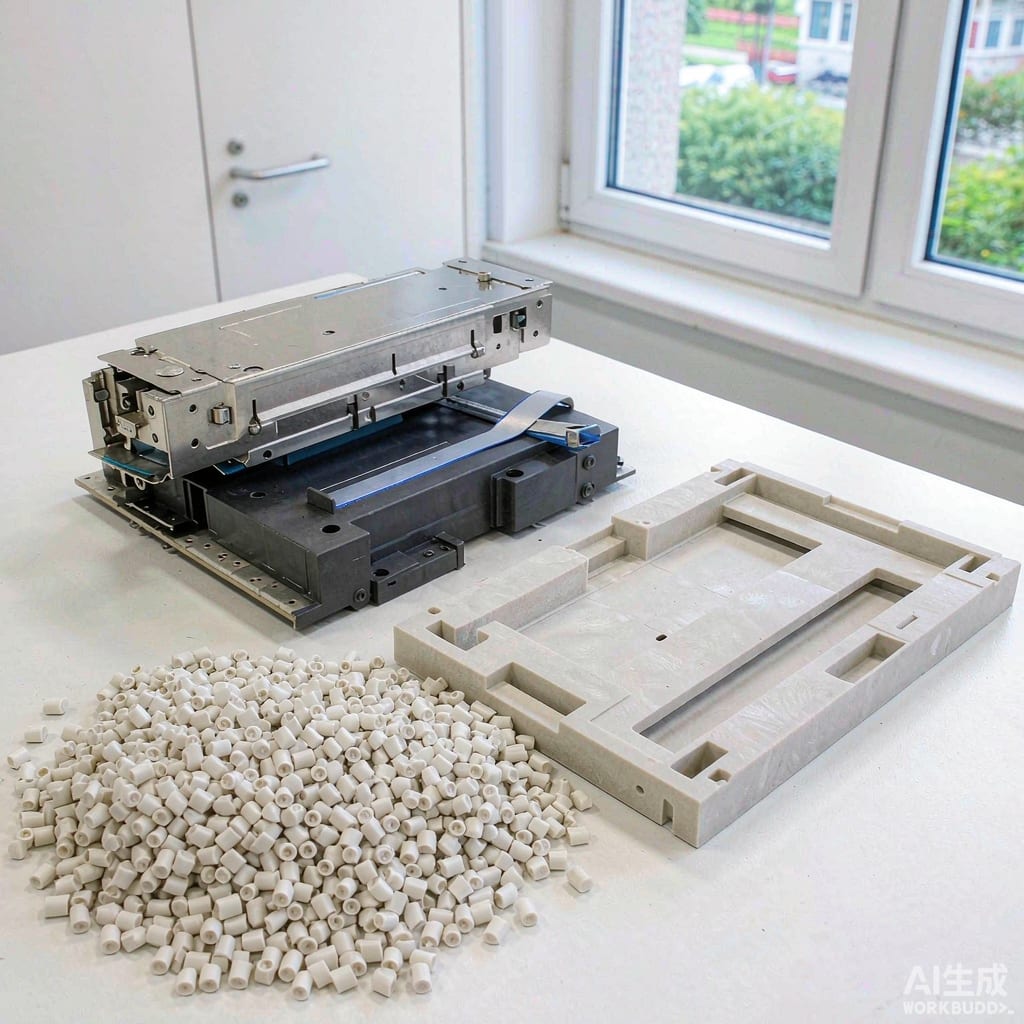
## Introduction
Surface-mount technology (SMT) reflow soldering exposes fixtures, carriers, and co
ector housings to peak temperatures of 245–260 °C. Ordinary engineering plastics such as ABS and unmodified PBT soften or warp under these conditions. For high-volume electronics manufacturing, materials that retain stiffness, dimensional accuracy, and chemical resistance at reflow temperatures are essential.
Polyphenylene sulfide (PPS) reinforced with glass fiber has become a leading choice for SMT reflow fixtures, high-temperature co
ectors, and under-hood electronic components. This article explains the properties that make PPS glass-fiber pellets suitable for these applications and compares PPS to competing materials.
## What Is PPS?
Polyphenylene sulfide is a semi-crystalline thermoplastic with a high melting point near 285 °C and a glass transition temperature around 85–95 °C. Its aromatic ring and sulfur linkages give it excellent chemical resistance, inherent flame retardancy, and good dimensional stability. Unfilled PPS is somewhat brittle, so it is almost always compounded with glass fiber, mineral fillers, or both to improve strength and impact resistance.
### Key Properties of 40% Glass-Fiber PPS
– Tensile strength: 180–220 MPa
– Flexural modulus: 12–16 GPa
– Heat deflection temperature at 1.8 MPa: 250–270 °C
– Continuous service temperature: 200–240 °C
– Flammability: UL94 V-0 without added halogens
– Water absorption: <0.05%
These values explain why PPS outperforms most other engineering plastics in reflow and under-hood environments.
## PPS in SMT Reflow Fixtures
### Thermal Stability During Reflow
Reflow fixtures, also called solder pallets or wave solder carriers, hold PCBs during the solder paste heating cycle. They must remain flat while the board is heated above 240 °C. PPS GF40 retains enough stiffness at these temperatures to prevent warping, which protects fine-pitch components from solder bridging or tombstoning.
### Chemical Resistance to Fluxes and Cleaners
Flux residues and aqueous cleaning chemistries attack many plastics over time. PPS resists acids, bases, solvents, and flux residues, giving fixtures a longer service life and reducing the frequency of replacement.
### Low CTE for Dimensional Accuracy
The coefficient of thermal expansion of PPS GF40 is roughly 20–25 × 10⁻⁶ /°C in the flow direction. This is low enough to maintain tight tolerances on locating pins and component pockets across the reflow temperature range.
## PPS in High-Temperature Co
ectors
### Co
ector Housings for LED Drivers and Power Supplies
LED drivers, server power supplies, and EV onboard chargers generate heat that raises co
ector housing temperatures above 150 °C. PPS housings resist deformation and maintain contact retention force under these conditions.
### Automotive Under-Hood Electronics
Under-hood sensors, control modules, and electric power steering controllers see temperatures up to 150 °C continuous with short excursions above 175 °C. PPS co
ectors withstand these conditions better than PA66, which absorbs moisture and loses stiffness, or PBT, which has a lower melting point.
## PPS vs Competing Materials
### PPS vs LCP
Liquid crystal polymer (LCP) offers even lower moisture absorption and excellent flow in thin walls, making it popular for miniature co
ectors. However, LCP is more expensive and can be anisotropic, causing warpage in larger parts. PPS is more cost-effective for larger fixtures and structural housings.
### PPS vs PA66 GF30
PA66 glass-fiber reinforced is cheaper than PPS and has good toughness, but it absorbs moisture and softens around 250 °C. For reflow fixtures and high-temperature co
ectors, PA66 is generally unsuitable.
### PPS vs PBT GF30
PBT is easier to process and has good electrical properties, but its melting point near 225 °C limits use in lead-free reflow. PBT may survive a few reflow cycles but will deform over repeated thermal exposure.
## Processing Tips for PPS Pellets
PPS requires a melt temperature of 300–340 °C and a mold temperature of 130–160 °C to achieve good crystallinity and surface finish. Drying the pellets at 130–150 °C for 3–4 hours before molding is essential to avoid hydrolytic degradation. Mold design should include adequate venting because PPS has low melt viscosity and can trap air in complex geometries.
## Conclusion
PPS glass-fiber pellets deliver the heat resistance, dimensional stability, chemical resistance, and flame retardancy needed for SMT reflow fixtures and high-temperature co
ectors. While LCP excels in miniature parts and PA66 offers lower cost, PPS remains the practical workhorse for applications where lead-free reflow temperatures and long-term thermal endurance are non-negotiable.



