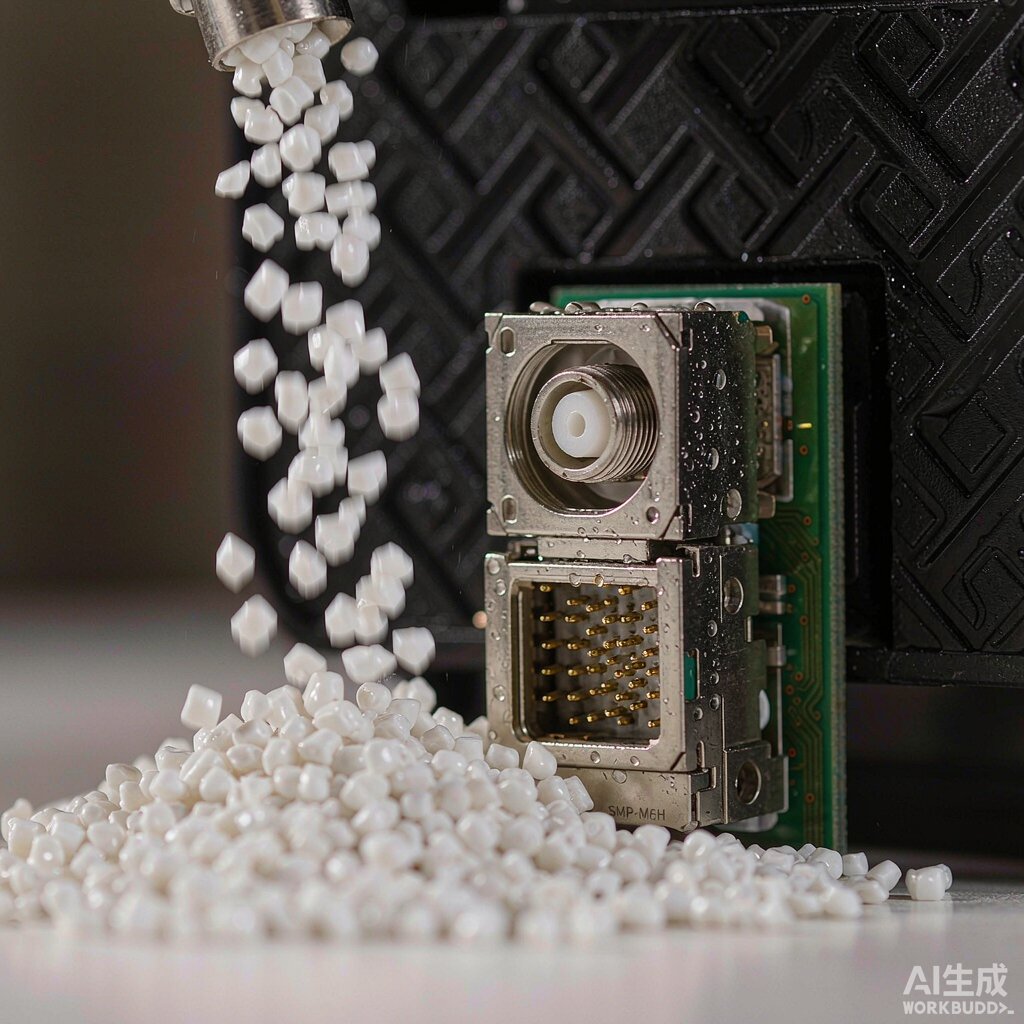
Every high-speed SMT co
ector on a modern board, from 25 to 112 Gbps chip sockets to ante
a modules and floating shield co
ectors, is almost certainly molded from liquid crystal polymer. No other engineering pellet combines stable electricals at gigahertz frequencies with the heat endurance to survive reflow at these tolerances. Here is what LCP is, why co
ector designers keep choosing it, and how to mold it without fighting its quirks.
What Makes LCP Different
LCP belongs to the family of liquid crystal polymers: its rigid, rod-like molecular chains stay ordered even in the melt, flowing in aligned domains rather than as coiled spaghetti. This ordered flow gives LCP its signature properties of extremely low melt viscosity, near-zero mold flash, low shrinkage, and strong anisotropy, because the chains orient along the flow direction and stiffen the part in that direction.
For co
ectors, the practical consequences are thin walls of 0.15 to 0.30 mm that still fill completely, flat parts that stay flat, and copy-to-copy consistency that keeps contact pitch true across a two-thousand-cavity mold.
The Electrical Case for LCP
Dielectric Constant and Loss at Frequency
Unfilled LCP grades run a dielectric constant of about 2.9 to 3.5 and a dissipation factor of 0.002 to 0.004 at 10 GHz, figures that remain stable across temperature and humidity because the polymer absorbs almost no water, less than 0.04 percent at saturation. Glass- and mineral-filled grades shift Dk upward slightly but hold the low loss. For impedance-controlled co
ector geometries, that stability across reflow temperature and a humid week in Southeast Asia is worth more than an extra decimal of low loss on a datasheet.
Comparison Against Rival Resins
- PPS: excellent heat and chemical resistance, but a dissipation factor around 0.004 to 0.01 and higher moisture uptake push it out of the fastest designs.
- PA9T and PA46: tough and reflow-capable, but dielectric constant above 3.7 and higher water absorption limit their use in millimeter-wave modules.
- PBT GF30: an economical workhorse for general co
ectors, yet its water absorption and mid-range electricals confine it to lower frequencies.
LCP is not always the answer. Its brittleness, since unfilled grades are notably less tough than nylon, and its price keep PPS and polyamides alive in many sockets. But where signal integrity rules, LCP wins.
Heat Resistance for SMT Reality
Co
ector housings reflow together with the board. LCP melts between 280 and 335 degrees Celsius depending on grade and holds useful mechanical properties far past 230, so a lead-free reflow profile with 245 to 260 degree peaks leaves the housing unmoved. Continuous-use ratings around 200 to 240 degrees also cover automotive under-hood positions. One caution: unfilled LCP softens enough above its glass transition that contact normal forces should be validated at temperature, not assumed from room-temperature spring data.
Molding Guidelines
- Drying: LCP absorbs little water, but surface moisture causes drool and silver streaks. Dry two to four hours at 120 to 150 degrees and keep hopper humidity low.
- Melt temperature: follow the grade window, typically 300 to 350 degrees for type II resins. Too cold and weld lines turn brittle; too hot and degradation blackens the melt.
- Mold temperature: 70 to 120 degrees. Warmer molds improve weld-line strength and surface finish; cold molds trap oriented skin layers that warp thin parts.
- Injection speed: fast fill exploits the low viscosity, but excessive speed causes jetting and gas burns in thin sections. Tune in small increments.
- Venting: LCP fills so readily that trapped air flashes before it voids. Deep, polished vents at 0.01 mm or less prevent both burns and flash.
Anisotropy and Weld Lines: The Two Real Hazards
Because the chains orient along flow, shrinkage is two to three times higher across flow than along it, and thin rectangular parts predictably bow. Countermeasures include symmetric gating, deliberate flow leaders rather than guesswork, and mold-flow analysis before cutting steel.
Weld lines are the second hazard. Where two flow fronts meet, the oriented skins fail to knit and the weld can be dramatically weaker than bulk material. Place welds away from contact beams and snap hooks, or vent and reheat the convergence zone deliberately. For precision co
ectors, a weld-line pull test belongs in first-article inspection.
Choosing a Grade
- Unfilled: maximum flow and lowest loss for ante
a-in-package and RF micro parts, at the cost of brittleness.
- Mineral filled, thirty to forty percent: the co
ector industry default, with balanced shrinkage, good weld strength, and stable electricals.
- Glass filled, thirty percent: highest stiffness and heat deflection for chip carriers and sockets, with more anisotropy to manage.
- Low-Df specialty grades: for 28 GHz and above and automotive radar, where even standard LCP loss is too high.
Specifying LCP is ultimately a packaging decision: a resin that stays electrically quiet through reflow and a decade of humidity is what allows a co
ector to meet its cha
el budget on the last day of its life, not just the first. Buy pellets against a written property table covering dielectric constant and loss at frequency, water absorption, and heat deflection, and the rest of the design falls into place.



