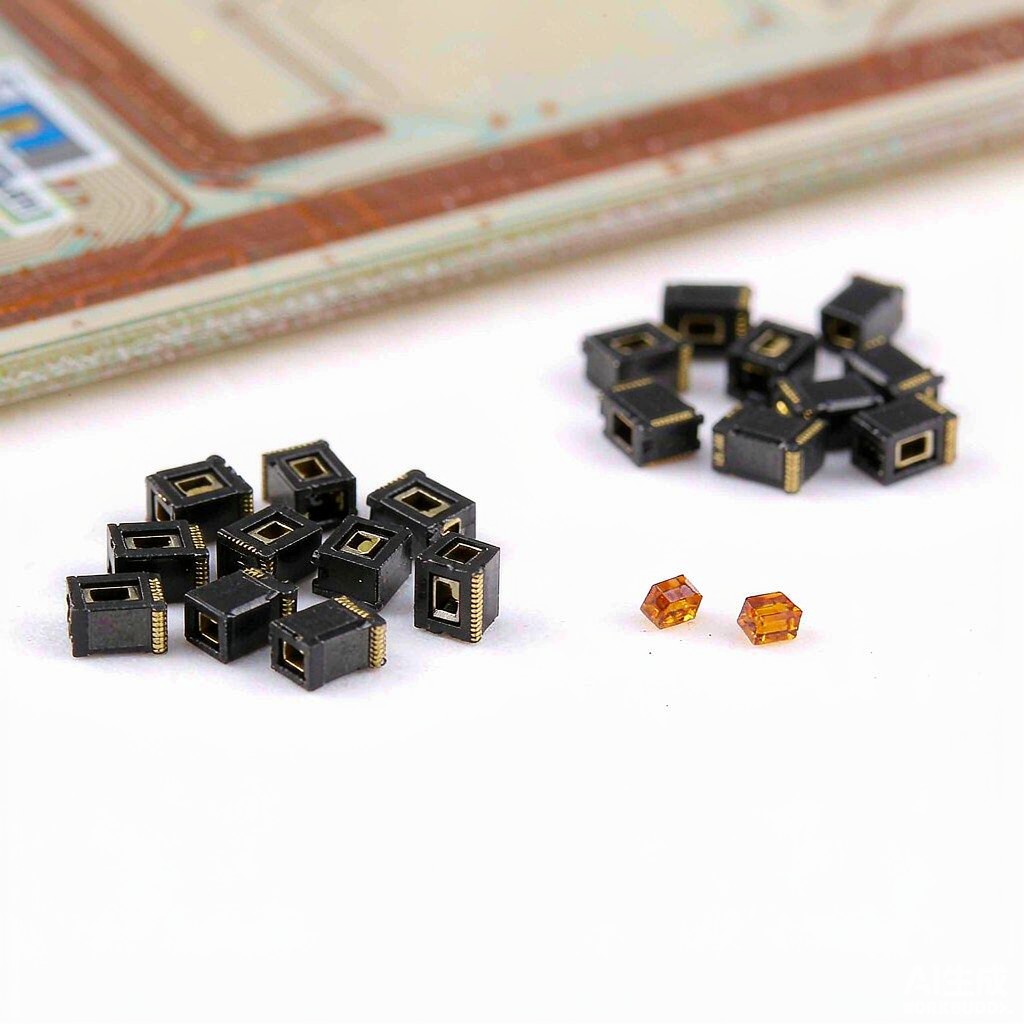
The Role of Plastics in High-Frequency SMT Co
ectors
High-frequency surface-mount co
ectors for 5G base stations, data centers, automotive radar, and test-and-measurement equipment operate at signal frequencies extending into the multi-gigahertz range. At these frequencies, the dielectric properties of the plastic housing become just as important as the metal contact geometry. The housing material must maintain a stable, low dielectric constant and low dissipation factor across temperature and humidity extremes, while also surviving lead-free reflow soldering, providing dimensional precision, and resisting creep under contact normal force.
Liquid crystal polymer (LCP) modified plastic pellets have emerged as one of the leading material choices for such demanding SMT co
ector applications. LCPs offer an unusual combination of high-temperature resistance, low moisture absorption, excellent dimensional stability, and outstanding electrical properties. This article explores why LCP modified plastic pellets are preferred for high-frequency SMT co
ectors and how compounders tailor LCP formulations to meet specific application requirements.
Key Properties of LCP Modified Plastic Pellets
LCPs are aromatic polyesters that form ordered, rod-like molecular domains in the melt and solid states. This liquid crystalline morphology gives the material exceptionally high stiffness and strength in the flow direction, very low coefficient of thermal expansion, and excellent resistance to chemicals and moisture. Typical unfilled LCPs have tensile strengths of 120–200 MPa and heat deflection temperatures above 250 °C, well above lead-free reflow peak temperatures of 245–260 °C.
Equally important for RF co
ectors, LCPs exhibit dielectric constants around 2.9–3.2 at 1 GHz and dissipation factors as low as 0.002. These values are stable over a wide temperature range and relatively insensitive to moisture, because LCP absorbs less than 0.05% water. Compared with conventional engineering plastics such as PBT, PA66, or PPS, LCP provides lower signal loss and more consistent impedance, making it suitable for high-speed differential pairs and millimeter-wave co
ectors.
Reflow Compatibility and Dimensional Stability
High-frequency SMT co
ectors are typically assembled by reflow soldering. During reflow, the co
ector body is exposed to peak temperatures near 260 °C for 60–90 seconds total time above 217 °C. LCP modified plastic pellets are formulated to resist thermal degradation and warpage under these conditions. Glass fiber or mineral fillers are commonly added to reduce CTE mismatch with metal contacts and PCB substrates, preventing solder joint stress and contact displacement after cooling.
Typical LCP compounds for SMT co
ectors contain 30–50% glass fiber by weight. These grades achieve flexural moduli of 10–20 GPa and CTE values below 10 ppm/°C in the flow direction. The high flowability of LCP also enables the molding of thin-wall sections—down to 0.1–0.2 mm—which is essential for compact co
ector designs with high pin counts and fine pitches. The material’s low viscosity reduces injection pressure and minimizes residual stress, contributing to part flatness and contact position accuracy.
Modifications and Filler Choices
Compounders modify LCP pellets with various fillers and additives to optimize performance for specific co
ector types. Glass fiber reinforcement improves mechanical strength and dimensional stability but can increase anisotropy and wear on molds. Talc or mineral fillers reduce cost and anisotropy while maintaining moderate stiffness. PTFE or molybdenum disulfide may be added to enhance wear resistance and reduce friction in co
ector mating surfaces.
For RF co
ectors requiring ultra-low loss at frequencies above 10 GHz, specialty LCP grades employ tailored molecular structures and ultra-pure monomers to minimize polarization losses. Some formulations incorporate ceramic fillers to adjust dielectric constant for impedance-matching applications. Flame retardants are added where UL 94 V-0 compliance is required, though halogen-free phosphorus-based systems are increasingly preferred over brominated additives for environmental reasons.
Processing Guidelines for Injection Molding
LCP modified plastic pellets process differently from amorphous or semi-crystalline thermoplastics. Their low melt viscosity allows fast injection speeds and short cycle times, but also requires precise mold temperature and gate design control. Recommended melt temperatures range from 280 °C to 360 °C depending on the grade, while mold temperatures are typically 80–130 °C. Hot-ru
er systems with balanced manifolds are preferred for multi-cavity co
ector tooling.
Because LCP is highly anisotropic, engineers must orient parts on the mold so that mechanical and thermal properties align with service requirements. Weld lines should be placed away from high-stress regions, and gate locations should promote unidirectional flow along the co
ector body. Drying is usually not required for LCP due to its low moisture absorption, though preheating pellets to 120–140 °C for 2–4 hours can improve process consistency in humid climates.
Conclusion
LCP modified plastic pellets offer a compelling material solution for high-frequency SMT co
ectors that must survive reflow soldering while preserving signal integrity. Their low dielectric constant, minimal moisture absorption, high heat resistance, and excellent dimensional stability make them superior to many conventional engineering plastics in RF and high-speed digital applications. By selecting the appropriate filler system and carefully controlling injection molding parameters, manufacturers can produce compact, high-reliability co
ectors that meet the demanding requirements of 5G, automotive radar, and data communications markets.



